One-Year Results of a Chemical Plant's Ultrapure Water SystemOne-Year Results of a Chemical Plant's Ultrapure Water System
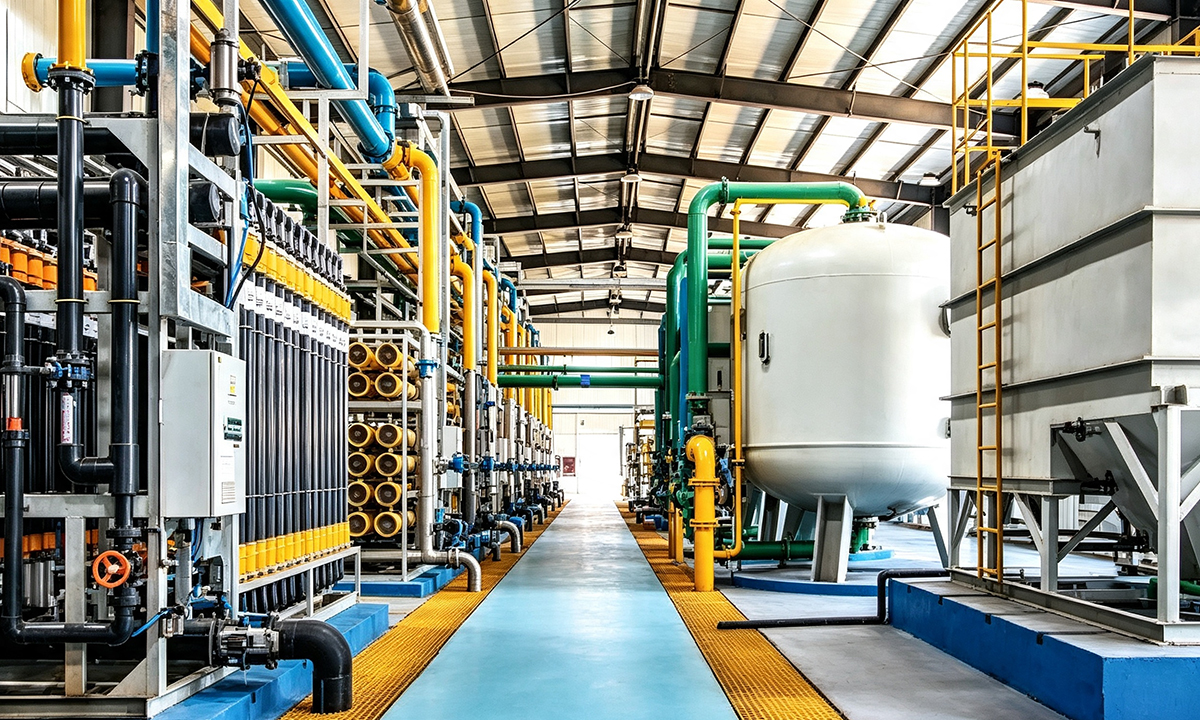
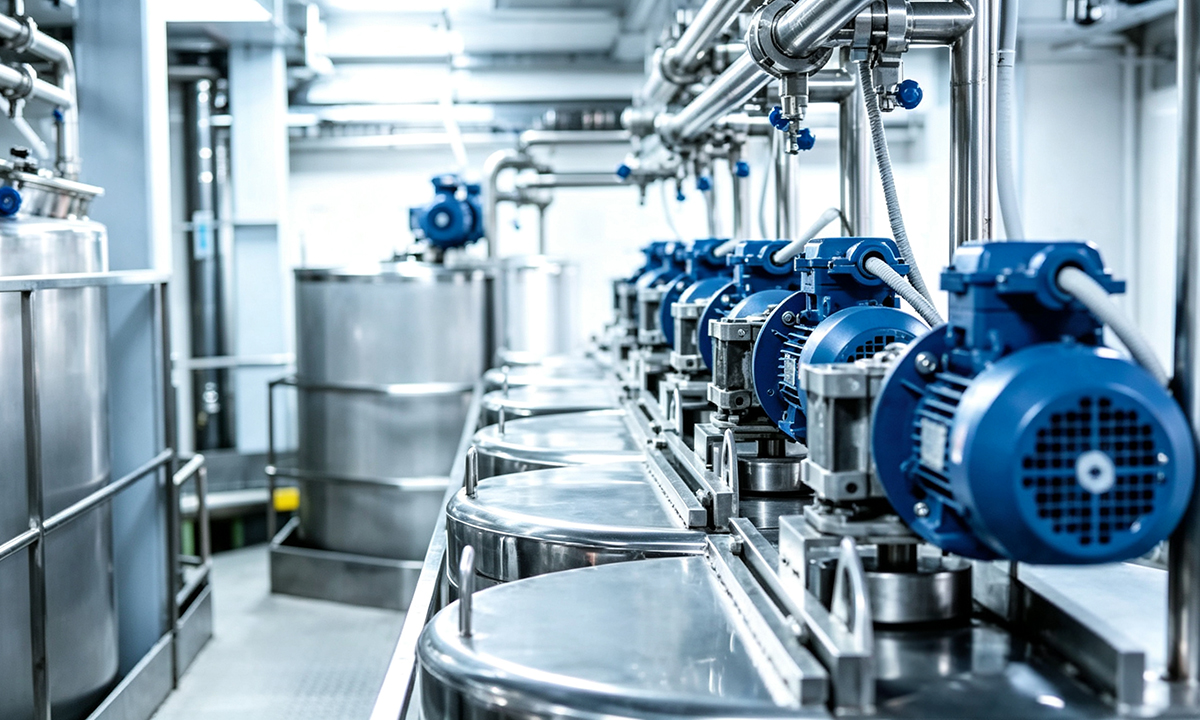
The company has long been dedicated to providing high-standard industrial water purification solutions for the chemical industry. Last year, we undertook an ultrapure water system upgrade project for a mid-sized chemical plant. The client, primarily engaged in fine chemical production, was struggling with significant fluctuations in product water quality and frequent membrane fouling in their existing water treatment system.